Advanced Engineering Consultancy & Testing Laboratory
Centre for Advanced Testing, Inspection and Engineering Solutions
Advanced Engineering Consultancy & Testing Laboratory
Centre for Advanced Testing, Inspection and Engineering Solutions
Learn when should PMI testing be used to verify alloy grade, prevent material mix-ups, support code compliance, and protect critical assets for safe service.
A stainless steel spool can look identical whether it is specified as 316L, 304L, or a lower-alloy substitute. Once it is welded into a corrosive process line, however, the consequences of an incorrect grade may include premature corrosion, unplanned shutdowns, costly replacement, and a difficult compliance investigation. That is when should PMI testing be used becomes a practical engineering question rather than a quality-control formality.
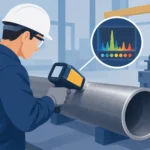
Positive material identification (PMI) testing verifies the elemental composition of an alloy and compares the result with the material grade specified for the component, weld, or assembly. It is commonly performed using portable X-ray fluorescence (XRF) analyzers, optical emission spectrometry (OES), or laboratory chemical analysis where a higher level of certainty is required. The right timing and scope depend on the material, service conditions, governing code, traceability available, and consequences of failure.
PMI testing should be used whenever material identity is critical to safety, corrosion resistance, mechanical performance, code compliance, or contractual acceptance. It is particularly valuable where visual identification, color coding, or paperwork alone cannot provide sufficient confidence that the installed material matches the design specification.
The highest-priority applications are typically pressure-retaining systems, structural components in demanding environments, high-temperature equipment, corrosion-resistant piping, and fabricated assemblies containing multiple alloy grades. In these applications, a single material mix-up can compromise an otherwise compliant design.
PMI is not necessarily required on every piece of commodity steel. For low-risk, clearly traceable materials used in noncritical service, the cost and effort may outweigh the benefit. The decision should be based on risk: what happens if the wrong material is installed, how likely is a mix-up, and can the material be reliably traced from receipt through fabrication and installation?
Incoming material verification is one of the most effective uses of PMI. It confirms that plates, pipe, fittings, flanges, bar, valves, and other purchased items are consistent with purchase requirements before they enter production.
Mill test reports are essential records, but they do not physically prove that each item on the shop floor corresponds to the certificate presented. Material can be incorrectly labeled, separated from its documentation, mixed during storage, or supplied under an incorrect tag. PMI at goods receipt provides an independent check before cutting, machining, and welding add value to potentially incorrect material.
This approach is especially appropriate when materials arrive from multiple suppliers, are stored in shared laydown areas, or include visually similar grades. Common examples include 304/304L and 316/316L stainless steel, carbon steel and low-alloy steel, duplex and super duplex stainless steels, nickel alloys, and chrome-moly steels.
Fabrication introduces several opportunities for material control to fail. Offcuts may be returned to storage without clear identification. Components may be moved between work areas. Assemblies can contain a combination of base metals, cladding, overlay, weld metal, and purchased fittings. PMI provides a direct method of verifying that the correct alloys remain in the correct locations.
Testing during fit-up is particularly useful before permanent joining obscures access or makes replacement expensive. A risk-based inspection plan may call for PMI of each pressure-containing component, a defined percentage of repetitive items, or 100% testing of higher-risk alloy systems. The appropriate sampling rate should be agreed in the inspection and test plan rather than selected after fabrication is complete.
PMI can also support weld consumable control. For corrosion-resistant and high-temperature applications, weld deposit chemistry must be compatible with the base material and service environment. Depending on the method used, PMI can verify key alloying elements in the deposited weld metal. Where carbon content, nitrogen, or other light elements are critical, OES or laboratory analysis may be more appropriate than XRF.
Final PMI verification is often justified before equipment is installed or placed into service, particularly where repair after commissioning would require shutdown, excavation, confined-space entry, or major disassembly.
For a piping system, final checks may focus on accessible valves, flanges, fittings, branch connections, and spool identification. For pressure equipment, the scope may include shells, heads, nozzles, supports, internals, and repair areas. The objective is not simply to produce test readings. It is to establish defensible evidence that critical components match the approved material schedule and are traceable to their location.
This stage is also valuable when project documentation is incomplete, when components have been stored for an extended period, or when material has changed hands between fabricator, contractor, and asset owner. PMI records can close traceability gaps before responsibility transfers at handover.
Certain conditions raise the value of material verification substantially. PMI should be strongly considered when alloys are selected for corrosion resistance, elevated-temperature strength, low-temperature toughness, sour service, or chemical compatibility. The more narrowly the design depends on a specific composition, the less acceptable it is to rely on appearance or unverified documentation.
In oil and gas, chemical processing, water treatment, mining, marine, power generation, and transport infrastructure, PMI is frequently applied to components exposed to chlorides, acids, caustics, high temperatures, cyclic loads, or aggressive process media. A substitution that appears minor on paper can materially change resistance to pitting, stress corrosion cracking, sulfidation, oxidation, or hydrogen-related damage.
PMI is also prudent after repairs, modifications, or failure events. Replacement parts may have been sourced under time pressure. Repair welds may involve different consumables. If a failure investigation indicates unexpected chemistry or material substitution, expanded PMI can help define the extent of the issue across similar assets.
Portable XRF is fast, nondestructive, and well suited to identifying many alloy families through key elements such as chromium, nickel, molybdenum, manganese, copper, and certain other metals. It is highly effective for sorting and verifying stainless steels, nickel alloys, and many low-alloy steels in field and fabrication environments.
However, XRF has limitations. It generally cannot reliably measure carbon and may not be suitable when distinction depends on light elements or tightly controlled composition ranges. For example, differentiating between low-carbon and standard stainless grades may require supporting documentation or another analytical method. Surface coatings, paint, scale, contamination, and curvature can also affect readings.
OES can measure carbon and other elements that may be outside the capability of handheld XRF, but it requires surface preparation and creates a small burn mark. Laboratory chemical analysis may be necessary for dispute resolution, certification, failure analysis, or situations where the material specification requires a complete compositional assessment.
Method selection should therefore be tied to the acceptance criteria. A fast XRF screening program is not equivalent to full chemistry certification, and it should not be represented as such. Qualified personnel should define which elements must be verified, the acceptable grade range, surface preparation requirements, test locations, and reporting format before testing begins.
A useful PMI program starts with the material specification and the asset risk, not with the instrument. The plan should identify components requiring verification, the applicable drawings or material classes, selected test method, acceptance criteria, sampling frequency, and treatment of nonconforming results.
Clear location control matters as much as chemistry. Each result should be linked to a unique component or weld location, its drawing reference, heat number where available, date, operator, instrument identification, and calibration status. Photographs and marked-up isometrics can be valuable for complex assemblies. Without this traceability, a technically sound reading may have limited value during audit, handover, or later investigation.
If an indication does not match the specified alloy, the correct response is not automatically to reject the part. The result should be reviewed against the applicable specification, confirmed where necessary using a suitable method, and assessed by competent engineering personnel. The investigation may identify a labeling error, an acceptable equivalent material, surface contamination, instrument limitation, or a genuine material substitution requiring containment and replacement.
Accredited testing and inspection services add confidence where results will support regulatory, contractual, or safety-critical decisions. AECTL applies qualified personnel, calibrated equipment, documented procedures, and multidisciplinary materials expertise to help clients define practical PMI scopes and interpret results in the context of service conditions and asset integrity.
The best time to plan PMI is before material arrives, fabrication starts, or a shutdown window closes. Treat it as targeted verification at the points where a material error is easiest to prevent and most expensive to discover later.